 Made in USA
Static electricity damages electronic components by discharging energy through sensitive structures such as gate oxides and semiconductor junctions. The discharge often occurs at voltage levels the operator never feels. Its most expensive consequence is latent degradation, which passes final test but surfaces in the field.
This article explains how electrostatic discharge (ESD) physically damages components and why latent failures cost more and are harder to detect than catastrophic ones. It then covers what the per-incident cost range means in practice. Finally, it shows where relative humidity (RH) fits as a facility-level prevention variable.
Key Takeaways
The points below summarize the mechanism, the cost, and the facility-level prevention layer this article covers. Each one is expanded in the sections that follow.
- Electrostatic discharges can destroy MOSFET gate oxides and degrade semiconductor junctions at voltages below 100 volts. People generally begin to notice a static shock between about 1,000 and 2,000 volts.
- Latent ESD failure is a distinct failure mode from catastrophic failure. The component passes final electrical test but carries partial oxide degradation. That degradation causes early-life field failure, often within the first year of deployment.
- The JEDEC Human Body Model classification, originally published as JESD22-A114 and now superseded by ANSI/ESDA/JEDEC JS-001, ranks components by ESD sensitivity. Its scale runs from Class 0 (damaged below 250 volts) to Class 3B (8,000 volts and above). Whichever device is most sensitive in an assembly sets the control floor for the entire production environment.
- ESD-related losses are estimated at $100 to $10,000 or more per incident in direct costs. Total program exposure rises substantially when warranty claims, field return logistics, and failure analysis labor are included.
- ANSI/ESD S20.20 and IEC 61340-5-1 are the primary ESD control program standards for electronics manufacturing. Many defense, aerospace, and automotive supply contracts treat conformance as a qualification requirement rather than a best practice.
- Maintaining RH between 40 and 60 percent reduces the surface resistivity of materials. ESD Association guidance confirms that humidity helps reduce charge accumulation. It complements grounding, wrist straps, and ionization controls rather than replacing them.
What Static Electricity Actually Does to an Electronic Component
Static charge builds up on surfaces and personnel through the triboelectric effect. Whenever two dissimilar materials touch and then separate, electrons move from one surface to the other. The exchange leaves one surface positively charged and the other negatively charged.
Dry air prevents that charge from dissipating in a production environment. When a charged person or object contacts a component, current flows through the lowest-resistance path available. That current delivers energy to structures not designed to absorb it.
Three structure types are the primary failure sites in electronic components. The list below names each one and the devices that rely on it.
- Gate oxides: MOSFETs and CMOS devices are exposed through their gate oxides.
- p-n junctions: Diodes and bipolar transistors are exposed through their p-n junctions.
- Thin-film conductor traces: Integrated circuits are exposed through their thin-film conductor traces.
The Triboelectric Effect in Production Environments
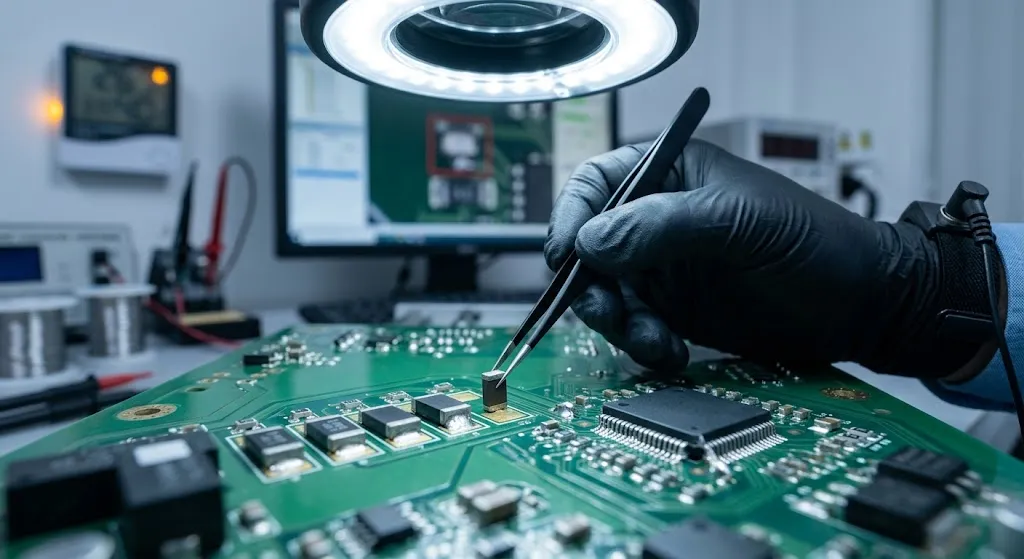
Sliding components across foam and handling plastic bags both generate significant triboelectric charge. Removing boards from non-conductive packaging and walking on non-conductive flooring add to that charge. None of this reflects operator carelessness, because the charge is a matter of physics that occurs however carefully personnel handle components.
Why Low Humidity Makes Static Buildup Worse
Dry air is a poor conductor of surface charge. Without a moisture film, charge on a surface has no slow path to dissipate. It builds until a discharge event occurs.
Surface resistivity is the humidity-dependent measure of how readily a material lets charge move across it. That measure rises sharply as humidity falls. The effect becomes most consequential in facilities operating below 30 percent RH.
Catastrophic vs. Latent ESD Failure: Why the Distinction Matters
Catastrophic ESD failure is immediate. Final test catches these failures, because the component stops working at the moment of discharge. The cost therefore stays bounded to the defective unit plus rework labor.
Latent ESD failure differs in every respect that matters to your cost structure. A component with partial degradation such as oxide thinning, junction weakening, or increased leakage current can still pass final electrical test. It then ships and operates normally at first.
Normal operating stress gradually overwhelms the degraded structure. Eventually, the device fails in the field, often within months. The cost of that failure includes the warranty claim and field return logistics, plus failure analysis labor and potential customer relationship damage.
Latent failures are harder to catch and costlier to close out than catastrophic ones. The IEC 61340-5-1 standard provides the formal requirements for an ESD control program meant to guard against catastrophic and latent damage alike. Below, the two modes are compared on the dimensions that affect a quality program.
- Detectability at final test: Catastrophic failures are caught at test. Latent failures pass test.
- Time-to-failure: Catastrophic failures are immediate. Latent failures emerge in early field life, often within the first year.
- Cost profile: Catastrophic failures carry per-unit and rework costs. Latent failures add warranty, return logistics, and failure analysis.
- Root-cause attribution: Catastrophic failures trace back to production quickly. Latent failures are frequently misattributed to design or assembly variation.
Why Latent Failures Pass Final Test
Standard functional tests apply controlled electrical conditions that a partially damaged gate oxide may still tolerate. In the field, that same oxide faces sustained operating stress, temperature cycling, and voltage transients over time. As a result, final test pass rate is not a reliable indicator of ESD program effectiveness when latent damage is present in your production environment.
The Cost Profile of Each Failure Type
The $100 to $10,000 per incident range for ESD-related losses represents direct per-unit costs. At the high end, the range almost always involves latent failures traced back to the production environment after a field return cycle. Although catastrophic failures are expensive, latent failures cost more and are harder to close out.
Component Sensitivity Thresholds: How Little Voltage It Takes
People generally begin to notice a static shock between about 1,000 and 2,000 volts. By contrast, CMOS and MOSFET devices belong to the many components that can be damaged by discharges below 100 volts. Some Class 0 devices are damaged at less than 250 volts as well.
That gap is why "we used wrist straps and never felt a shock" does not constitute an ESD control program. The JEDEC Human Body Model classification, originally published as JESD22-A114 and now superseded by ANSI/ESDA/JEDEC JS-001, gives a device-level framework for assessing risk. Classes run from most to least sensitive in the list below.
- Class 0: Devices in this class are damaged below 250 volts.
- Class 1A: The sensitivity range is 250 to 499 volts.
- Class 1B: Sensitivity here runs from 500 to 999 volts.
- Class 1C: The range for this class is 1,000 to 1,999 volts.
- Class 2: Devices in this class fall between 2,000 and 3,999 volts.
- Class 3A: Sensitivity runs from 4,000 to 7,999 volts.
- Class 3B: Devices in this class are damaged only at 8,000 volts and above.
JEDEC Classification and What It Means on the Production Floor
Every component in a design can be assigned an ESD sensitivity class. The most sensitive device in any assembly sets the floor for all ESD control measures across that production environment. A circuit board with one Class 0 device anywhere in its bill of materials must be handled with Class 0-level precautions at every stage.
Why Modern Components Are More Sensitive, Not Less
Shrinking geometries and falling operating voltages have made modern components more sensitive to ESD, not less. Thinner gate oxides require less discharge energy to rupture. ESD programs built for component generations from ten or fifteen years ago may be systematically under-protective for current production, however adequate they once were.
The Real Cost of ESD in Electronics Manufacturing
ESD-related costs are routinely underreported because standard defect tracking captures catastrophic failures at final test but not latent failures that manifest in the field. The $100 to $10,000 per incident range represents direct per-unit exposure. Total program exposure across a facility handling hundreds of thousands of components per year is a different order of magnitude.
Several cost components typically fall outside those per-incident estimates. The list below names four of them.
- Failure analysis labor: Field returns require engineering time to trace each failure back to its cause.
- Warranty administration and logistics: Every returned unit adds administration and return logistics cost.
- Customer penalty clauses: Field defect rates can trigger penalties under customer contracts.
- Supplier corrective action requests: In regulated supply chains, an ESD event that reaches the customer can trigger a request that costs far more than the defective unit.
Defect Rate Data and Production Yield Impact
ESD events that cause catastrophic failures reduce direct production yield. Latent failures distort quality metrics because the defect rate measured at final test doesn't reflect the rate delivered to the customer. A first-year field return rate that consistently exceeds the final test defect rate can indicate latent ESD damage in production, not only design variation.
Compliance and Contractual Exposure
ANSI/ESD S20.20 and IEC 61340-5-1 conformance is a contractual requirement in many defense, aerospace, and automotive supplier agreements. MIL-STD-1686C applied specifically to ESD control in military electronics manufacturing until the Department of Defense cancelled it in 2021. ANSI/ESD S20.20 and ESD TR20.20 replaced it.
For suppliers in these chains, non-conformance can void supplier qualification and trigger audit requirements. Treating ESD control as a best practice rather than a compliance obligation creates contractual exposure that legal and quality teams may not have fully assessed.
Facility-Level Prevention: Where Humidity Fits in the ESD Control Stack
Standard ESD control programs operate at the workstation level through grounding mats, wrist straps, and conductive footwear. Ionizers and anti-static packaging join them as valid and necessary controls. All of these address the discharge at or near the point of contact.
None of them addresses the environmental condition that allows charge to accumulate in the first place. Relative humidity shapes that condition directly through its effect on surface resistivity. At low RH, insulating surfaces hold charge almost indefinitely.
Within 40 to 60 percent RH, a moisture film on surfaces enables slow charge dissipation before the charge reaches discharge thresholds on most material types. That film is why humidity control lowers the background rate of static buildup across the facility. With fewer and weaker discharge events reaching workstation-level controls, humidity makes grounding and ionization more effective rather than replacing them.
Why Dry Air Is an ESD Risk Factor, Not Just a Comfort Issue
Facilities in low-humidity climates routinely operate below 30 percent RH during peak static seasons. The same happens in facilities that run aggressive heating, ventilation, and air conditioning (HVAC) cooling without humidity makeup. At those levels, charge dissipation is negligible.
Even normally acceptable materials become significant static generators under these conditions. Winter heating, cleanroom HVAC, and refrigerated production areas are common places where RH drops without deliberate measurement. Dry air is an ESD risk factor that deserves the same measurement discipline as grounding.
Humidity Control as a Systemic ESD Risk Reduction Strategy
Maintaining facility RH within 40 to 60 percent using precision humidification addresses ESD risk across the entire production environment at once. That matters most where workstation controls are hardest to enforce consistently across every person and process step. Large assembly facilities, printed circuit board (PCB) manufacturing lines, and semiconductor handling areas fit that description.
In those settings, a facility-level approach through electronics manufacturing humidification complements per-workstation measures. For a deeper look at the yield impact in PCB production, see how low humidity increases PCB defect rates.
How Smart Fog Addresses ESD Risk at the Facility Level
Smart Fog ESD control systems use compressed air and water through a proprietary nozzle to produce an equal-sized droplet grid. Those droplets self-evaporate before reaching any surface. Under proper system design, that lets the system raise RH into the 40 to 60 percent band without wetting surfaces.
A humidification system that wets racks, PCBs, or assembly fixtures creates a different set of failures than it prevents. Direct exposure to the fog stream will still wet a surface. System design must therefore account for fog stream placement relative to components and personnel.
Non-Wetting Humidification for Sensitive Electronics Environments
Self-evaporating droplets deliver humidity without surface wetting under proper system design. This suits PCB manufacturing floors and component handling areas where surface moisture is unacceptable. Placing a hand or object directly in the fog stream will wet it.
The same requirement applies to facilities that use cleanroom humidifiers. Steam systems can deposit condensate on cool surfaces. Ultrasonic systems can leave mineral residue behind.
By contrast, Smart Fog droplets evaporate into the air instead of settling. For more detail, see humidity and ESD control in PCB manufacturing facilities on facility-specific application and PCB manufacturer humidification for PCB production system configurations.
Precision and Continuous Operation for Electronics Manufacturing
Precision matters when the target is a specific RH band for ESD mitigation. Smart Fog systems maintain humidity up to 99 percent RH with plus or minus 1 to 2 percent precision. A facility targeting 50 percent RH therefore stays within specification continuously, not just on average.
Holding that precision around the clock calls for 24/7 set-and-forget operation. With no moving parts in the humidification process and maintenance intervals up to every two years, intervention stays minimal. That matters in facilities where humidification downtime is not acceptable.
Beyond the equipment itself, each installation is delivered as a complete engineered system, not a component kit. The broader program context is covered in our guide to preventing static electricity in electronics manufacturing. A side-by-side look at prevention approaches is available in our ESD control methods comparison piece.
Final Thoughts
ESD damage in electronics manufacturing falls into two categories with fundamentally different cost profiles. Catastrophic failures are visible, detectable at test, and bounded in cost. Latent failures are invisible at the point of manufacture, pass final inspection, and generate their full cost in the field.
The voltage thresholds at which damage occurs are far below the threshold of human perception. Program design therefore can't rely on operator sensation as a proxy for control effectiveness. That is why facility conditions belong in the control stack alongside workstation controls.
Facility-level humidity control within the 40 to 60 percent RH range reduces the rate of static charge buildup across the entire production environment. It complements grounding, ionization, and workstation-level controls. Where that layer is absent or uncontrolled, the ESD risk profile is higher than per-workstation controls alone can address.
If your facility handles ESD-sensitive components, precision humidity control is worth evaluating as part of your ESD risk reduction program. To discuss system design for your production environment, contact Smart Fog engineers.
FAQ
Can static electricity damage electronics without the operator feeling a shock?
Yes, static electricity can damage electronic components without the operator feeling anything. People generally begin to notice a static shock between about 1,000 and 2,000 volts. Many component families, including CMOS and MOSFET devices, are damaged by discharges below 100 volts. An operator handling a component can therefore cause a damaging ESD event with no sensory warning.
Is ESD damage to electronic components always permanent?
ESD damage to electronic components is typically permanent. Even partial damage, such as gate oxide thinning in a MOSFET, does not self-repair after a discharge event. The degraded structure either fails immediately or operates with reduced tolerance until normal operating stress causes early-life failure in the field.
What is the difference between a latent ESD failure and a catastrophic ESD failure?
Catastrophic ESD failure is immediate and detectable at final test, unlike latent ESD failure, which passes final test and surfaces in the field. Latent failures involve partial degradation such as oxide thinning or junction weakening. The total cost of a latent failure runs higher because warranty claims, field return logistics, and failure analysis labor add to the component cost.
At what voltage does static electricity begin to damage electronic components?
Some CMOS and MOSFET devices are damaged by discharges as low as 10 to 100 volts, depending on the device. Under the JEDEC Human Body Model classification, now published as ANSI/ESDA/JEDEC JS-001, Class 0 devices are damaged below 250 volts. People generally begin to notice a static shock between about 1,000 and 2,000 volts. Significant damage can therefore occur well before an operator perceives any discharge.
How does low humidity increase the risk of ESD damage in manufacturing?
Low humidity increases ESD risk by reducing the ability of surfaces to dissipate static charge. Insulating surfaces without a moisture film hold charge until a discharge occurs. Facilities operating below 30 percent RH see more static buildup. Grounding and ionization controls must then intercept more frequent and larger discharge events.
What standards govern ESD control programs in electronics manufacturing?
ANSI/ESD S20.20 and IEC 61340-5-1 are the primary standards governing ESD control programs in electronics manufacturing. MIL-STD-1686C governed military electronics production until the Department of Defense cancelled it in 2021. ANSI/ESDA/JEDEC JS-001 classifies component ESD sensitivity by Human Body Model voltage. Many defense, aerospace, and automotive suppliers treat conformance with ESD control standards as a condition of staying qualified.
How do you get rid of static electricity in an electronics manufacturing facility?
Static electricity in an electronics manufacturing facility is controlled by layering several measures, because no single control eliminates it. Grounding mats, wrist straps, and conductive footwear protect individual workstations. Ionization systems neutralize charge on surfaces that can't be grounded. Facility-level humidity control between 40 and 60 percent RH lowers the charge accumulation rate that workstation-level controls must manage.
Is static electricity harmful to PCBs that have already passed final test?
Yes, a PCB that has passed final test can still carry latent ESD damage from earlier handling. Components on the board may have suffered partial gate oxide degradation or junction weakening that final test conditions did not stress enough to expose. Degraded components can then fail in the field under sustained operating stress. A high final test pass rate therefore doesn't confirm the absence of latent ESD damage in the production environment.