 Made in USA
When relative humidity (RH) drops in a print facility, paper loses moisture unevenly across its fiber structure. The resulting dimensional distortion, curl, and added stiffness are the direct mechanical cause of both paper jams and registration errors.
This article traces each step in that causal chain as a distinct, named failure mode. It also identifies the RH thresholds where problems begin. Finally, it explains how continuous humidity control restores the dimensional stability that print production needs.
Key Takeaways
- Paper conditioning standards such as TAPPI T 402 and ISO 187 set 50% RH, plus or minus 2%, as the standard conditioning atmosphere for paper. Against that benchmark, fiber shrinkage becomes measurable below 40% RH and operationally significant below 35% RH.
- Curl from moisture loss isn't uniform. Grain direction decides which axis shrinks more. Long-grain and short-grain paper therefore curl in different directions and fail at the feeder in predictable ways.
- Paper jams from low humidity come from three mechanically distinct failure modes: curl-induced misfeed, static-induced multi-sheet feed, and stiffness-induced path failure.
- Multi-pass registration error is a separate failure mode from paper jams. It occurs when a sheet loses more moisture between print passes and no longer matches the geometry laid down in pass one.
- Indoor RH in heated facilities drops to 15 to 25% in winter, as cold outside air is warmed without added moisture. Low-humidity jam cycles are therefore seasonal and preventable.
- Static electricity in dry conditions makes sheets cling together until printers pull several at once. The resulting multi-sheet jams happen at the feeder, not further along the paper path.
- Paper moved from cold storage into a warm, dry print room needs 24 to 48 hours of acclimation before loading. Skipping that step brings on curl and feed failures, whatever the facility-wide RH.
What Happens to Paper When Humidity Drops
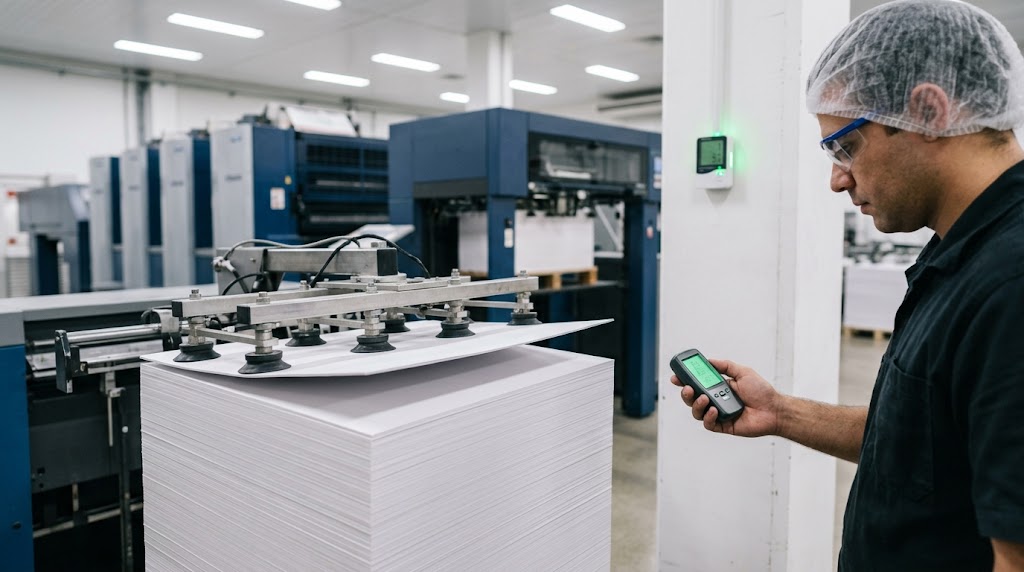
Paper is hygroscopic, meaning it absorbs moisture from the surrounding air when RH rises and releases it when RH falls. That exchange doesn't happen evenly across a sheet or a ream. Because the exposed edges of a stack give up moisture before the interior does, the sheet dries unevenly and curls instead of shrinking flat.
Fiber orientation adds a second layer to this. Fibers running with the grain hold their dimensions better under moisture loss than fibers running across it, which means cross-grain shrinkage outpaces along-grain shrinkage when humidity drops. The resulting curl follows a direction you can predict from the paper type and how the ream was cut.
Moisture loss leaves paper with four distinct physical changes. Each one is worth knowing by name:
- Curl: Differential shrinkage between the sheet face and edges lifts the sheet out of a flat plane.
- Dimensional shrinkage: The sheet becomes physically smaller across the cross-grain axis.
- Edge waviness: Moisture loss concentrated at the edges creates a wavy perimeter.
- Increased stiffness: Drier fibers lose flexibility. The sheet then needs more force to navigate curves in a paper path.
Why Paper Curls Rather Than Shrinks Flat
A sheet's exposed surface dries faster than its interior fibers. The interior resists the shrinkage happening at the surface. Tension between the two bends the sheet instead of contracting it evenly.
Grain direction amplifies the effect. Because cross-grain fibers respond more strongly to moisture loss, the curl follows an axis set during manufacturing. Short-grain and long-grain paper curl in different directions, and to different degrees, under the same humidity drop.
The RH Threshold Where Physical Change Becomes Operationally Significant
Two paper standards anchor the numbers here. TAPPI T 402 and ISO 187 set 50% RH, plus or minus 2%, as the standard atmosphere for conditioning and testing paper and board. A related method, TAPPI T 502, covers how to measure the equilibrium relative humidity of paper.
Against that 50% benchmark, fiber shrinkage becomes measurable below 40% RH. Below 35% RH, the shrinkage grows large enough for feed mechanisms and registration systems to detect. Those are the numbers that mark when a humidity problem turns into a production problem.
How Low Humidity Causes Paper Jams
Low-humidity paper jams come from three mechanically distinct failure modes. These can occur on their own or together. The jam location is a useful diagnostic signal, because each mode jams the printer in a different place.
Here's how the three compare:
- Curl-induced misfeed: A curled sheet doesn't lie flat in the feed tray. The separator roller either misses it or feeds it in at an angle. The jam happens at tray pickup.
- Static-induced multi-sheet feed: Electrically charged sheets stick together. The separator pulls two or more at once as a unit. The jam happens at the feeder or input stage.
- Stiffness-induced path failure: Paper that has lost moisture becomes stiff enough to resist the curves of the internal paper path. It jams mid-path, at a bend or turn.
Static Electricity as a Separate Jam Mechanism
When RH drops, air loses its ability to dissipate surface charge. Sheets of paper build up static electricity until they stick together. The separator mechanism then pulls several of them through as a single unit, and the result is a multi-sheet jam at the feeder.
Jam location is what tells a static jam apart from a curl-induced misfeed. Static jams happen at the feeder input, whereas curl jams usually happen at tray pickup. For facilities managing ongoing static problems, ESD control systems address this failure mode alongside humidity correction.
Why Winter and Heating Cycles Predict Jam Frequency
Cold outside air holds very little absolute moisture. When a heating, ventilation, and air conditioning (HVAC) system draws that air in and warms it, RH drops sharply without any change in absolute moisture content. Indoor RH in heated facilities commonly falls to 15 to 25% in winter.
Jam frequency tracks this pattern closely. Facility managers who recognize it can schedule humidity interventions before peak jam season instead of reacting to mid-run production stops.
How Low Humidity Causes Registration Errors in Multi-Pass Printing
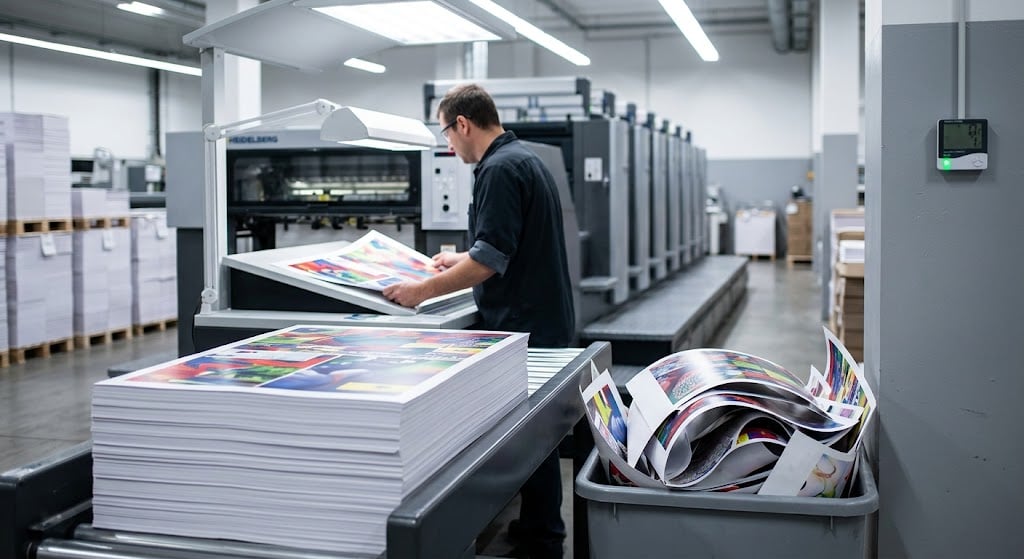
Registration errors and paper jams aren't the same problem. A jam is a feed and transport failure, whereas a registration error is a dimensional accuracy failure that only happens in multi-pass printing. In a two-pass digital or offset run, the press lays down one color separation on the first pass and expects the sheet to come back at identical dimensions for the second.
Trouble starts when the sheet loses moisture to dry ambient air between those passes. Its physical dimensions change. The press registration system, however, is still working from the original geometry. That mismatch produces three visible signs of misregistration:
- Color halos: Separations sit slightly off one another around images.
- Blurred edges: Lines and shapes lose their sharp outline.
- Doubled text: Type appears to print twice, slightly offset.
Because print tolerances in commercial offset and digital work are tight, even a fraction of a millimeter of change across a large sheet is enough to cause visible misregistration.
That's also why pre-conditioning paper before a run doesn't solve the problem on its own. A sheet equilibrated to 50% RH that then sits in a 30% RH pressroom for 20 minutes between passes starts losing moisture and changing dimensions before pass two even begins. What prevents misregistration is continuous RH control throughout the run.
How Grain Direction Compounds Registration Error
Paper's dimensional response to moisture loss is greater across the grain than along it. A drying sheet therefore shrinks more in one axis than the other. In multi-pass printing, that directional shrinkage makes misregistration worse along one axis.
That pattern doubles as a diagnostic. If misregistration is worse in one direction than the other with no change in press calibration, grain-direction shrinkage from humidity loss is a primary suspect.
Digital vs. Offset: How Registration Sensitivity Differs by Process
Offset presses using physical plates hold tighter registration tolerances than single-pass digital workflows. That makes them more sensitive to dimensional change between passes.
Toner-based digital presses running duplex jobs are also susceptible, because the sheet passes through the imaging unit twice. Any moisture loss between those passes affects toner adhesion and image alignment. The printing process your facility runs determines how much dimensional drift you can tolerate before misregistration shows.
Operational and Storage Factors That Make Low-Humidity Jams Worse
Humidity affects paper before it ever reaches the press. Three operational factors consistently make low-humidity problems worse:
- Paper acclimation: Paper moved from cold storage or a delivery vehicle into a heated, dry print room needs 24 to 48 hours to equilibrate before loading. Without that time, the surface dries faster than the interior can adjust. Curl sets in before a single sheet is printed. This step is documented in paper manufacturer conditioning guidelines and grounded in TAPPI T 402 conditioning procedures.
- Ream storage: Unopened reams protect paper from ambient RH swings. A ream opened in a dry room and left exposed overnight measurably shifts moisture content before the next print run.
- Tray loading: Overfilled trays give statically charged sheets less room to separate in dry conditions. Keeping trays at 50 to 70% capacity reduces contact area between sheets. That lowers the incidence of static-induced multi-sheet pulls.
These measures manage the symptoms. They don't address the root cause, which is ambient RH deficiency across the print environment.
Why Paper Storage Conditions Matter Before the Print Run
Paper stored in a conditioned room at 50% RH and moved straight into a 30% RH pressroom starts losing surface moisture immediately, even before loading. Facilities with a dedicated conditioned paper store next to the press floor manage this transition more effectively. Those receiving paper from uncontrolled warehouses have a harder time.
For more on how temperature and humidity interact to affect paper handling across a facility, see ideal humidity levels for printing facilities.
How Precision Humidity Control Restores Dimensional Stability in Print Facilities
Keeping paper dimensionally stable through a print run takes stable RH through the whole run. Conditioning individual sheets before loading isn't enough.
Smart Fog's equal-sized droplet grid produces self-evaporating droplets that raise ambient RH and hold it within plus or minus 1 to 2% continuously. That precision removes the humidity fluctuation between passes that causes dimensional drift. For printing facility humidity control, this level of stability is what stops registration error at its root.
Smart Fog systems also run without constant nozzle cleaning or daily maintenance. That matters in production, where humidity control has to stay reliable across a full shift without anyone managing it.
Static dissipation and dimensional stability both depend on the same continuous RH set point. That's why humidity and static control in industrial printing rooms go hand in hand.
Non-Wetting Humidification in Paper-Sensitive Environments
Standard misting or spray-based humidification brings a surface-wetting risk that doesn't suit paper handling. Wet droplets landing on paper stock, feed trays, or print heads cause more damage than low humidity itself.
Self-evaporating droplets humidify the air rather than surfaces. Under proper system design, ambient RH rises to the set point with paper, rollers, and print heads staying dry. Direct exposure to the fog stream, such as placing a hand in it, will still produce wetting.
Continuous RH Precision Across the Full Print Run
The dimensional stability benefit depends on RH staying consistent through the whole run, not just at the start. The RH a sheet sees in pass one has to match the RH it sees on re-entering the press for pass two.
Smart Fog humidity control systems hold a set point continuously. The environment between passes is therefore the same one that existed during pass one. That's exactly the condition that prevents inter-pass dimensional drift and the registration errors it causes.
Low humidity affects more than registration, though. The guide on how low humidity causes print quality issues covers its effects on ink absorption, toner adhesion, and color consistency. Each follows from the same root mechanism.
Final Thoughts
Paper jams and registration errors share a root cause: ambient RH falling below the level where paper stays dimensionally stable. The failure modes, though, are distinct.
Jams come from physical sheet deformation that disrupts feed paths. Registration errors come from dimensional change between print passes that the press registration system can't accommodate.
Both problems are predictable and preventable. Seasonal heating cycles make low-humidity jam periods a calendar event. Grain direction makes the axis of worst misregistration identifiable.
Continuous precision RH control removes the inter-pass drift that no amount of pre-conditioning or operational adjustment can fully fix. Across the full range of humidity-related print quality failures, RH stability is the single upstream control point. For more, see improving print quality with proper humidity control.
If jams and registration errors keep recurring across your print runs, ambient RH deficiency is the likely root cause. Contact Smart Fog engineers to request a facility humidity assessment and a system specified to keep paper dimensionally stable throughout production.
FAQ
At what relative humidity level does paper start curling and causing jams?
Paper starts curling and causing jams once relative humidity falls below about 40%, the point where moisture loss becomes measurable. Below 35% RH, fiber shrinkage grows large enough for feed mechanisms and registration systems to detect. Paper conditioning standards TAPPI T 402 and ISO 187 set 50% RH, plus or minus 2%, as the standard conditioning atmosphere for paper and board. Facilities running well below that level operate in conditions that deform paper and raise jam frequency.
Why does my printer jam more often in winter than in summer?
Printers jam more often in winter because heated indoor air is far drier than summer air. Cold outside air holds very little absolute moisture. When your HVAC system draws that air in and warms it, RH drops sharply, often to 15 to 25%, without any change in absolute moisture content. Seasonal humidity drops are predictable. Humidity control can therefore address them before production stops.
What is the difference between a paper jam and a registration error in printing?
A paper jam is a feed and transport failure, whereas a registration error is a dimensional accuracy failure. In a jam, a deformed sheet disrupts the printer's feed path or transport mechanism. Registration errors only happen in multi-pass printing, when a sheet changes dimensions between passes and the second image no longer lines up with the first. The two failures have different causes, show up in different parts of the press, and need different fixes.
How does low humidity cause misregistration in multi-pass printing?
Low humidity causes misregistration in multi-pass printing by shrinking the sheet between passes. Each pass has to align precisely with the image laid down before it. A sheet that dries out in the interval no longer matches the size the registration system is calibrated to. Even a fraction of a millimeter of drift produces visible color halos and blurred edges in commercial offset and digital work.
Does paper grain direction affect how paper curls when humidity drops?
Yes, paper grain direction affects how paper curls when humidity drops. Fibers running across the grain shrink more under moisture loss than fibers running along it. Uneven shrinkage between the two directions makes the sheet curl along a predictable axis. Misregistration from humidity loss is also worse in one direction in multi-pass printing. That asymmetry helps confirm humidity, rather than press calibration, as the root cause.
How long does paper need to acclimate before loading it into a printer?
Paper moved from cold storage or a delivery vehicle into a heated, dry print room needs 24 to 48 hours to acclimate before loading. Skipping acclimation lets the sheet surface dry faster than the interior. Curl then sets in before the paper even reaches the feed tray. The practice is grounded in TAPPI T 402 conditioning procedures and documented in technical guidelines from paper manufacturers including Sappi and Domtar.
Can humidity control prevent color registration errors in offset and digital printing?
Yes, humidity control can prevent color registration errors in offset and digital printing when it's maintained continuously through the print run. Pre-conditioning alone isn't enough. A mismatch between the conditioning RH and the pressroom RH still lets the sheet drift out of shape between passes. Holding RH continuously at the set point used during pass one keeps the sheet's dimensions stable for the whole run.
Why do sheets of paper stick together and cause multi-sheet feeds in dry conditions?
Sheets of paper stick together in dry conditions because dry air can't dissipate surface electrical charge. Static electricity builds up on each sheet until the sheets cling at their surfaces. When the printer's separator tries to feed one sheet, it pulls the charged stack as a unit and jams at the feeder input. Curl-induced misfeeds are a separate failure mode that happens at tray pickup instead. Raising facility RH above 40% reduces static buildup and lowers multi-sheet feed incidence.