 Made in USA
Semiconductor fabs target 40 to 45% relative humidity (RH) as the accepted fab-wide baseline. That range isn't arbitrary, because it sits between two failure boundaries.
Below 30% RH, electrostatic discharge (ESD) risk rises sharply. Above 55 to 60%, moisture-related process contamination increases. Within that band, individual process zones need tighter tolerances depending on how sensitive each manufacturing step is.
This article breaks down humidity targets by fab stage and explains the physical mechanisms linking humidity deviation to specific failure modes. You'll also see which process environments need the tightest control, along with the standards frameworks that shape fab humidity specifications.
Key Takeaways
- Semiconductor fabs typically target 40 to 45% RH as a fab-wide baseline. Individual process zones can need tolerances as tight as ±1% RH at the tool level.
- Photolithography is the most humidity-sensitive standard fab process. Elevated humidity causes photoresist solvents to absorb atmospheric moisture, altering film thickness and degrading pattern resolution.
- Below approximately 30% RH, the surface moisture layer on insulating materials thins. This weakens the natural charge dissipation pathway and increases ESD risk for unshielded devices.
- Deposition processes, including chemical vapor deposition and physical vapor deposition, need stable ambient humidity to keep trace moisture out of process chambers. Trace moisture can introduce oxide defects or alter film stoichiometry.
- Humidity control tolerance of ±1 to 2% RH is needed in the most sensitive fab zones. Fluctuations beyond that range can shift process chemistry enough to move yield metrics outside specification limits.
- Packaging and final assembly carry the highest ESD vulnerability because completed devices are fully exposed. Humidity control is the only ambient-level mitigation that addresses charge accumulation at the source.
- Moisture-sensitive devices covered by IPC/JEDEC J-STD-033 need controlled moisture exposure during handling, packing, and storage. That standard gives facilities a compliance anchor for packaging zone specifications.
- SEMI standards and ASHRAE cleanroom guidance set the design frameworks within which fab humidity specifications are developed.
The Fab-Wide Baseline: Why 40 to 45% RH Is the Standard Starting Point
The 40 to 45% RH range reflects decades of process development across silicon fabrication environments. It balances two opposing risks, one at each end of the humidity scale:
- Below 30% RH: The thin moisture film that naturally coats insulating surfaces dissipates. That film is the main pathway through which electrostatic charge bleeds away. Without it, charge accumulates. ESD events then become far more likely.
- Above 55 to 60% RH: Condensation risk rises on precision optics and tool surfaces. Sensitive films absorb moisture. Partially processed wafers also become vulnerable to electrochemical corrosion.
The baseline sits within the broader HVAC design context set by ASHRAE 62.1 ventilation and indoor air quality standards. That standard's 2025 edition added new humidity control requirements. On the equipment side, SEMI S2 is the semiconductor industry's environmental, health, and safety guideline for manufacturing equipment.
Neither framework mandates a single fixed set-point for every facility. Both shape the design context in which site-specific humidity specifications are developed. Treating 40 to 45% as a starting point, not a universal rule, is the correct engineering posture.
Why RH Below 30% Creates ESD Risk
Dry air increases the surface resistivity of insulating materials by removing the adsorbed moisture layer that lets charge dissipate. Below approximately 30% RH, that dissipation pathway weakens significantly. Electrostatic charge then accumulates on tool surfaces, wafer carriers, garments, and device packages.
For unshielded wafers and processed devices, that accumulated charge is a direct yield and reliability threat. ESD damage is often latent. A device can pass electrical test at the fab and still fail under field conditions.
Why RH Above 60% Introduces Process Risk
Elevated humidity introduces a different set of risks. Research on photoresist coating processes has found chamber humidity to be among the most significant factors in resist thickness and thickness uniformity.
Moisture absorption by photoresist films alters their solvent balance and viscosity, which changes film thickness across the wafer. Condensation on precision optics in lithography tools causes focal plane shifts that degrade pattern resolution.
On partially processed wafers with exposed metal features, high humidity can accelerate electrochemical corrosion of interconnects and bond pads. The 40 to 45% RH baseline is bounded on both sides by real failure mechanisms, not by convention.
Humidity Requirements by Fab Stage
The fab-wide baseline is only a starting point. Three process environments operate at the edges of what general HVAC systems can reliably hold. Each has a distinct sensitivity profile, a tighter tolerance requirement, and a specific failure mode when conditions deviate.
Photolithography: The Most Humidity-Sensitive Stage
Photolithography lines are typically maintained within the 40 to 45% RH range, with tolerances as tight as ±1% RH at the tool level. The sensitivity comes from photoresist chemistry, which reacts to humidity at several points in the process.
During resist coating, elevated ambient humidity causes the resist solvent to absorb atmospheric moisture. The absorbed moisture changes film viscosity across the wafer, leaving the resist unevenly thick. Uneven thickness shifts the optical path length at exposure, degrading pattern resolution and pulling etched features away from design intent, which directly cuts yield.
Humidity affects lithography in three distinct ways, depending on the direction and the process step:
- High humidity during coating: Moisture absorbed by the resist solvent causes thickness variation, which degrades pattern resolution and yield.
- Low humidity in the bay: Below 35% RH, electrostatic charge can build on wafer carriers and reticles. That charge attracts airborne particulates to wafer surfaces. Inspection may not catch the resulting defects until post-etch review.
- Storage and pre-bake: Resist stored outside its specified humidity range can absorb or lose moisture. That changes its exposure characteristics before coating even begins.
Thin Film Deposition: Moisture Contamination in Process Chambers
Chemical vapor deposition (CVD) and physical vapor deposition (PVD) chambers are evacuated or purged with ultra-pure process gases during operation. Inside, the chamber runs well below any meaningful relative humidity level. The fab ambient around the tool still matters, though.
Moisture in the ambient environment can threaten the process in three ways:
- Wafer surface adsorption: Moisture can adsorb onto wafer surfaces before they enter the load lock.
- Load lock infiltration: Moisture can get in through load lock seals during transfer.
- Gas line contamination: Moisture can contaminate ultra-pure gas lines that aren't fully isolated from ambient conditions.
Trace moisture during thermal oxidation can alter oxide stoichiometry. It can also introduce interface state defects that affect transistor threshold voltage.
At the chamber level, humidity management moves from relative humidity to dew point measurement. For a plain-language explanation of the two metrics, see our explainer and comparison of dew point vs humidity.
The fab ambient target of 40 to 45% RH applies to the environment around the tool. Inside the chamber, a separate ultra-dry control regime applies, tracked in dew point terms rather than RH.
Packaging and Final Assembly: ESD Risk at the Device Level
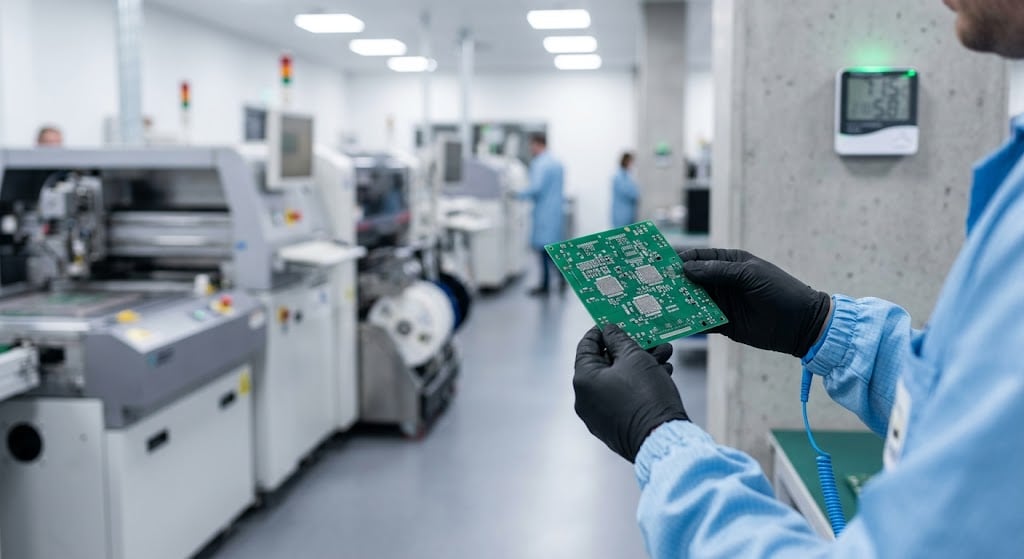
Packaging and assembly stages handle completed or nearly completed devices. These devices are fully exposed and at maximum ESD vulnerability.
At this stage, humidity serves mainly as an ESD safeguard rather than a process chemistry control. Packaging areas typically keep ambient RH above 40% to preserve the surface moisture layer on insulating materials.
That moisture layer targets the root cause of static: the absence of a charge dissipation pathway. This makes humidity the only ambient-level ESD control that works before charge builds up. Wrist straps, floor mats, and ionizers provide discharge paths only after charge has accumulated.
Moisture-sensitive devices bring a separate requirement. IPC/JEDEC J-STD-033 sets standardized methods for handling, packing, shipping, and using moisture/reflow-sensitive surface mount devices. Those methods help prevent damage from moisture absorbed before solder reflow, giving packaging zones a compliance anchor for moisture exposure.
What Happens When Humidity Deviates: Failure Modes by Direction
Humidity deviation failures often get misattributed. A process engineer investigating yield loss may look first at chemistry, tool calibration, or operator variation before environmental conditions.
Knowing which failure modes map to which deviation direction narrows root cause analysis faster. For a broader diagnostic framework, cleanroom humidity control standards and risks covers the standards context in more detail.
Failure Modes from Low Humidity (Below 35% RH)
Low-humidity failures are frequently latent. A device may pass all in-line electrical tests and appear to yield normally. Underlying damage can still surface later, during reliability screening or field operation.
- ESD-induced latent device damage: Charge accumulation below 35% RH can produce discharge events too small to cause visible physical damage. Those events can still degrade gate oxide integrity or metal interconnect reliability.
- Particulate adhesion from static charge: Electrostatic fields on wafer surfaces and carriers attract airborne particles. In a cleanroom running at low humidity, particle counts on wafer surfaces can increase even when filtration systems are working correctly.
- Resist adhesion failure: Inadequate ambient moisture during resist coating can affect the substrate interface, reducing adhesion uniformity and causing delamination during development or etch steps.
Failure Modes from High Humidity (Above 55% RH)
High-humidity failures are more likely to show up during inspection. Even so, they may be misattributed to process chemistry or tool variation when ambient humidity monitoring is inadequate.
- Photoresist film thickness variation: Solvent absorption at elevated humidity alters resist viscosity across the wafer. That thickness non-uniformity shifts critical dimension targets across the exposure field.
- Condensation on precision optics: Moisture on lens surfaces or reticles causes focal plane shifts and scattering effects. Pattern resolution then degrades in ways that resemble tool drift rather than environmental interference.
- Corrosion of exposed metal features: Partially processed wafers with exposed aluminum, copper, or tungsten interconnects are vulnerable to electrochemical corrosion. The risk rises when ambient humidity climbs above 55% during queue time between process steps.
Standards and Compliance Frameworks for Semiconductor Fab Humidity
Few published resources on semiconductor fab humidity bring the relevant standards frameworks together in one place. That gap matters for facilities engineers who need to tie their environmental control specifications to recognized external references rather than internal practice alone.
SEMI Standards Relevant to Fab Humidity
SEMI S2, the Environmental, Health, and Safety Guideline for Semiconductor Manufacturing Equipment, sets performance-based EHS considerations for semiconductor equipment. It applies to equipment used to manufacture, measure, assemble, and test semiconductor products. Its role is to define the equipment safety context, not a humidity set-point.
SEMI F21 classifies microelectronics clean environments by their airborne molecular contaminant (AMC) levels. Ambient humidity influences how molecular contaminants adsorb onto and desorb from wafer surfaces, which makes humidity control a relevant variable in AMC management.
Neither standard mandates a single fixed RH set-point. Both define part of the envelope within which facility-specific specifications must sit.
ASHRAE Cleanroom Ventilation and Humidity Guidance
ASHRAE 62.1 sets ventilation and indoor air quality requirements for heating, ventilation, and air conditioning (HVAC) system design in commercial and industrial facilities, including cleanrooms. Humidity control is addressed as part of contamination management and occupant protection.
For clean spaces specifically, ASHRAE Technical Committee 9.11 notes that cleanroom design covers far more than temperature and humidity. Its scope also spans particle, electrostatic discharge (ESD), molecular, and gaseous contamination control. Facilities engineers specifying humidity systems for semiconductor environments should treat ASHRAE guidance as a design input, not a regulatory minimum.
How Smart Fog Delivers ±2% RH Precision in Semiconductor Environments
Semiconductor fabs need humidity control tolerances as tight as ±1 to 2% RH at the most sensitive process stages. The humidification technology behind that must deliver stable, non-wetting performance without introducing particulate contamination or surface moisture into the cleanroom. Achieving both at once is the design constraint that defines which systems suit fab use.
Precision Without Surface Wetting
Smart Fog's equal-sized droplet grid is the mechanism behind non-wetting humidification. Every droplet carries a slight charge to prevent re-aggregation, then evaporates fully before reaching any surface. That allows precise humidity additions to fab air without moisture settling on equipment, racks, tool surfaces, or in-process wafers.
Non-wetting applies to surfaces under proper system design. Direct exposure to the fog stream, such as placing a hand directly into it, will wet that surface. Under designed installation conditions, the system adds humidity to the air without introducing liquid water into the cleanroom.
Key performance characteristics relevant to semiconductor fab environments:
- RH precision: Smart Fog systems maintain humidity up to 99% RH with ±1 to 2% precision, which suits photolithography bay and packaging zone requirements.
- 100% water efficiency: Every droplet evaporates into the air, so there's no pooling, no residual surface moisture, and no drainage requirement.
- Cleanroom compatibility: Self-evaporating droplets add no particulate load to the environment and leave no mineral deposits on surfaces or tool enclosures.
- Non-wetting operation: Surfaces remain dry under proper system design, which removes the condensation risk associated with some alternative humidification approaches.
For facilities evaluating ESD control systems as part of a broader environmental strategy, humidity is the ambient-level foundation that other ESD controls depend on. See also how humidity control prevents ESD in electronics manufacturing and ESD control methods compared for a fuller look at how ambient RH relates to ESD risk.
Continuous Fab Operation and Low Maintenance Demands
Semiconductor fabs run continuously. Humidity systems that need frequent nozzle servicing or manual intervention create scheduling conflicts with production.
Smart Fog systems avoid that, with no moving parts in the humidification process. Maintenance intervals extend up to every two years.
That design lets humidity control run as background infrastructure rather than a recurring maintenance item. The distinction matters in facilities where production schedules limit access to environmental systems.
For facilities with PCB manufacturer humidification requirements next to or within semiconductor packaging operations, the same non-wetting, low-maintenance architecture applies. Engineers evaluating system options can find more on electronics manufacturing humidification and cleanroom humidification systems.
Final Thoughts
Semiconductor humidity control isn't a single-specification problem. It's a stage-specific engineering challenge, where the consequences of deviation differ by process zone and by direction.
The 40 to 45% RH fab-wide baseline gives a defensible starting point. Photolithography, deposition, and packaging each need a more precise answer, tailored to the process chemistry and failure modes at that stage.
Engineers investigating yield issues or auditing environmental control systems now have a failure-mode taxonomy to apply diagnostically. It breaks down by deviation direction:
- Low humidity: This direction maps to ESD damage, particulate adhesion, and resist adhesion failure.
- High humidity: This direction maps to resist thickness variation, optics contamination, and interconnect corrosion.
Connecting observed defects to environmental conditions is faster when the causal mechanism is explicit.
For facilities engineers specifying humidity control systems for semiconductor manufacturing environments, contact Smart Fog engineers to discuss precision humidification designed for cleanroom-compatible, continuous fab operation.
FAQ
What is the recommended humidity level for a semiconductor cleanroom?
The recommended humidity level for a semiconductor cleanroom is 40 to 45% relative humidity. This range balances ESD risk below 30% RH against moisture-related contamination above 55 to 60% RH. Photolithography bays and other sensitive zones are often held tighter, to ±1% RH at the tool level. Site set-points should reflect SEMI and ASHRAE design frameworks alongside your own process window data.
Why does photolithography require tighter humidity control than other fab stages?
Photolithography requires tighter humidity control because photoresist chemistry is directly sensitive to ambient moisture. During resist coating, elevated humidity changes film viscosity and thickness uniformity across the wafer. Uneven resist thickness throws off the optical path length and blurs pattern resolution at exposure. Most lithography bays target 40 to 45% RH, with tolerances as tight as ±1% RH at the tool level.
What failure modes are caused by low humidity in semiconductor manufacturing?
Low humidity in semiconductor manufacturing mainly causes three failure modes: latent ESD damage, particulate adhesion, and resist adhesion failure. ESD events can degrade devices without leaving visible damage. Static charge also pulls airborne particles onto wafer surfaces, even in well-filtered cleanrooms. Low-humidity failures like these often stay hidden until electrical testing or reliability screening.
How does high humidity affect wafer yield in semiconductor fabs?
High humidity above 55% RH reduces wafer yield through resist thickness variation, optics condensation, and interconnect corrosion. Moisture absorbed by photoresist films changes their thickness and shifts critical dimension targets. Condensation on precision optics degrades pattern resolution. On partially processed wafers, exposed metal interconnects can corrode during queue time between process steps.
What SEMI standards govern humidity control in semiconductor fabrication facilities?
The two SEMI standards most relevant to fab humidity control are SEMI S2 and SEMI F21. SEMI S2 is the industry's environmental, health, and safety guideline for semiconductor manufacturing equipment. The second, SEMI F21, classifies clean environments by airborne molecular contaminant levels, which ambient humidity influences. Neither standard sets a single humidity number. Facilities build site-specific specifications within the frameworks both provide.
What is the difference between humidity control requirements for deposition versus packaging stages?
Deposition and packaging stages need humidity control for different reasons: contamination prevention in deposition, and ESD mitigation in packaging. Around deposition tools, the 40 to 45% RH ambient target keeps trace moisture off wafers and out of ultra-pure gas lines. Inside the chamber, conditions are ultra-dry and tracked by dew point instead. In packaging, ambient RH above 40% preserves the surface moisture layer that lets charge bleed off exposed devices.
Why does RH below 30% increase ESD risk in semiconductor environments?
RH below 30% increases ESD risk because the thin moisture film that normally lets charge bleed off insulating surfaces disappears. Without that film, charge builds up on tool surfaces, wafer carriers, garments, and device packages. That accumulated charge threatens unshielded devices and processed wafers. ESD damage at this level is often latent, surfacing only during reliability screening or field operation.
What humidity tolerance is required at the most sensitive semiconductor fab process stages?
The most sensitive semiconductor fab stages typically need humidity control tolerances of ±1% RH at the tool level. Those stages include photolithography bays and moisture-sensitive device handling areas. The broader fab ambient may be managed to ±2% RH. Holding those tolerances takes humidification systems designed specifically for that level of precision and stability.